OVERVIEW
The process is designed for long aluminum extrusion profiles joined to create the structural sections of high-speed railway vehicles.
Solution
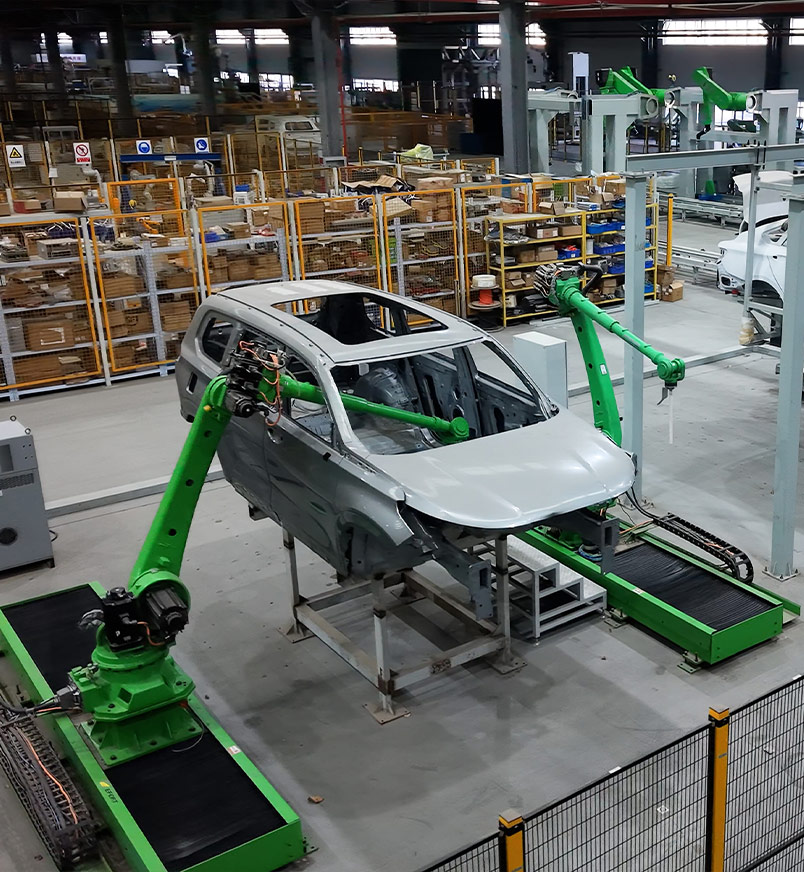
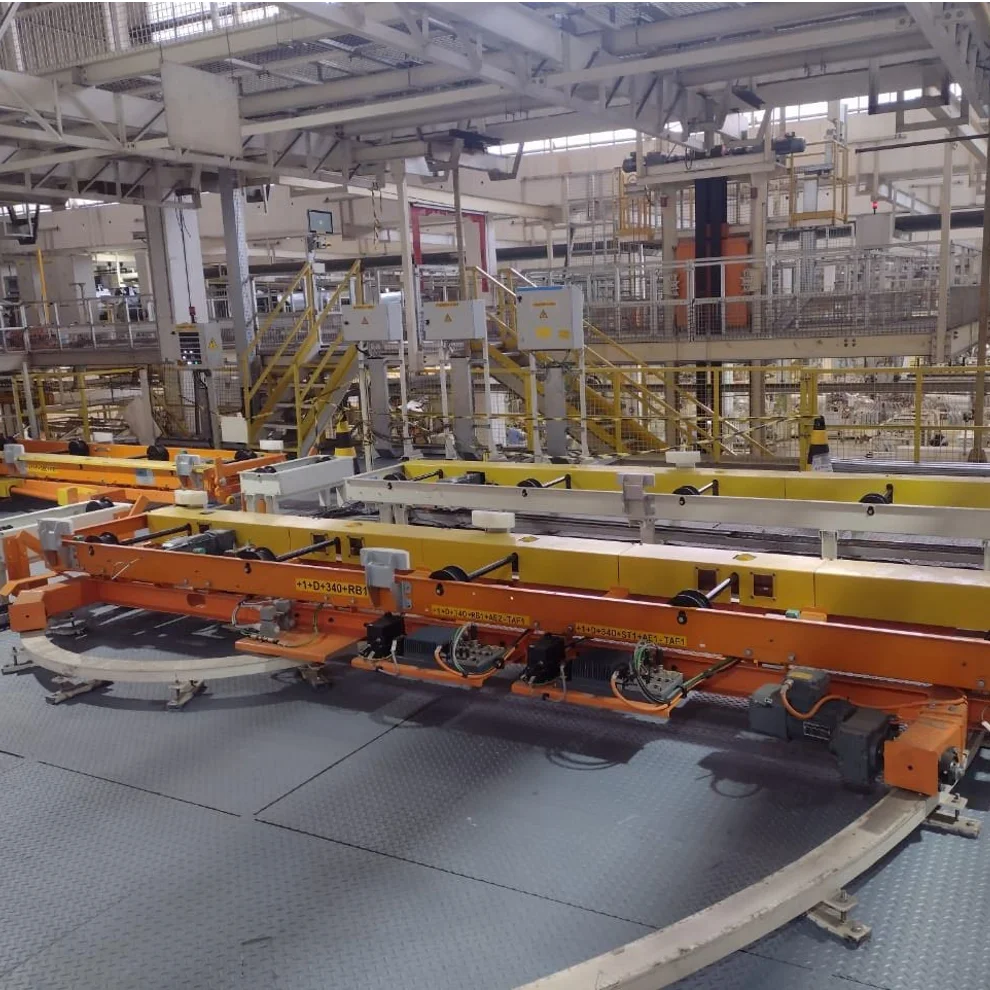
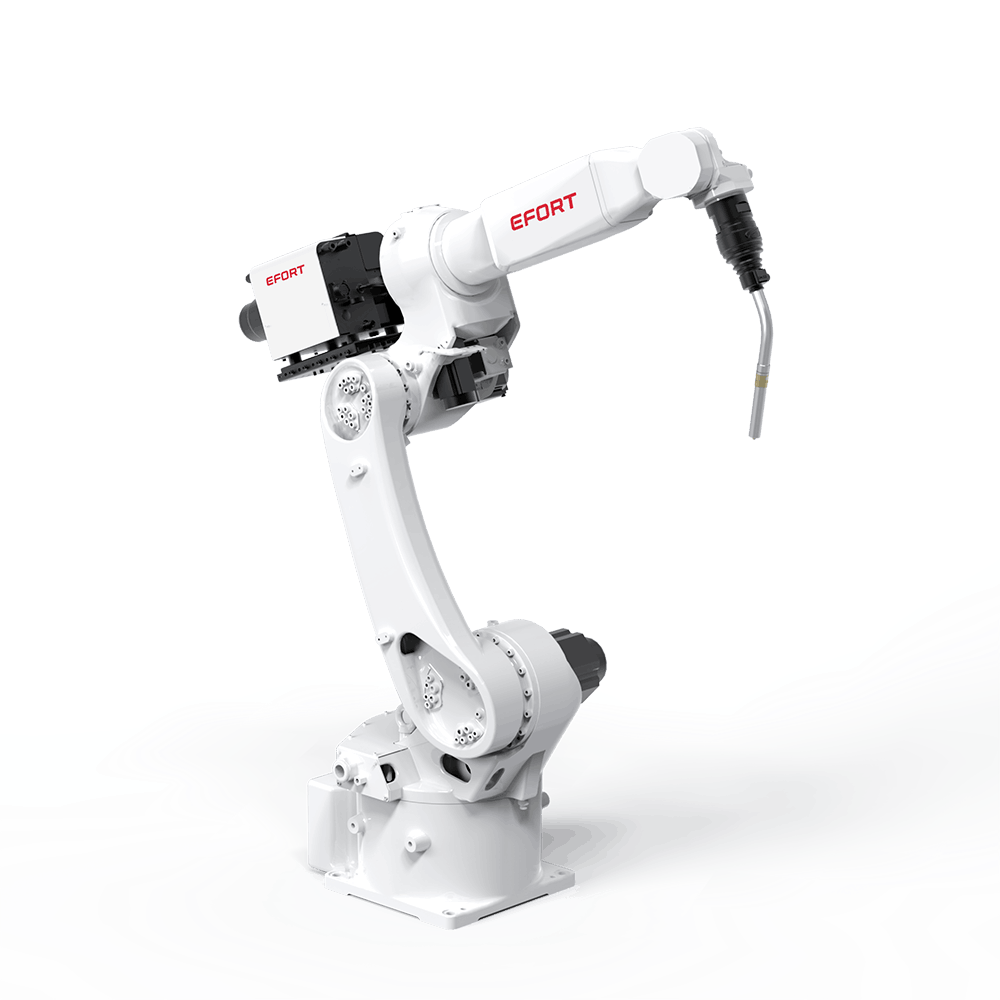
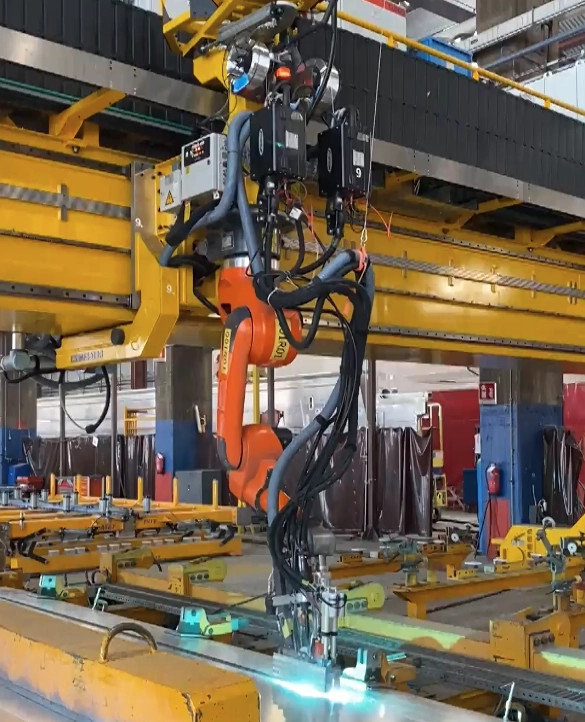
The system consists of an automatic gantry equipped with two arc-welding robots.
An integrated laser unit performs volumetric verification of the welding joint and supports instantaneous process correction.
Two additional robots perform brushing of the complete welded joints.
The complete architecture coordinates welding, joint verification, correction and finishing operations within one automated production concept.
Integrated joint verification and correction reduce the need for separate optical checks and limit downstream reworking operations.
The automated solution supports consistent welding quality across long structural components that would otherwise require extensive manual intervention.
- Automatic gantry-based production system;
- Two robotic arc-welding stations;
- Integrated volumetric joint verification;
- Laser-supported instantaneous correction;
- Automated welded-joint brushing;
- Reduced optical inspection requirements;
- Reduced reworking operations;
- Improved welding consistency;
- Suitable for large aluminum structures.
- Handling of approximately 25-metre aluminum profiles;
- Automatic arcwelding of long joints;
- Integrated joint inspection;
- Real-time correction support;
- Automated post-weld brushing;
- Coordinated gantry and robot motion.
Floors, bodysides and roofs manufactured from aluminum extrusion profiles for high-speed railway vehicles and other large, welded aluminum structures.